English (US)
 Español
 Deutsch
 Français
 Português
 Türk
 中国的
 ภาษาไทย
 Malay
TL;DR:
Knowing how to purge hot runner systems is essential for fast and thorough color and material changes in injection molding operations. Because hot runner systems keep plastic molten, contamination can linger longer than in cold runner setups, making the right purging approach critical for quality and efficiency.
- Why hot runner systems can be more challenging to purge than cold runner systems
- How molten plastic and low-flow areas contribute to color and material contamination
- Best practices for purging hot runner components safely and effectively
- How proper purging improves molded part quality and reduces scrap
- Tips for optimizing color and material changeovers without damaging hot runner parts
When done correctly, purging hot runner systems can lead to faster startups, cleaner transitions, and more consistent production results.
Hot runner systems are designed to improve efficiency, reduce waste and deliver high-quality molded parts. But when it comes time to change color or material, these same advantages can turn into challenges.
Because molten plastic stays heated inside the system, contamination can linger longer than it would in cold runner setups. Knowing how to properly purge hot runner systems is essential for clean changeovers, reduced scrap, and consistent part quality.
Understanding Hot Runner Systems vs. Cold Runners
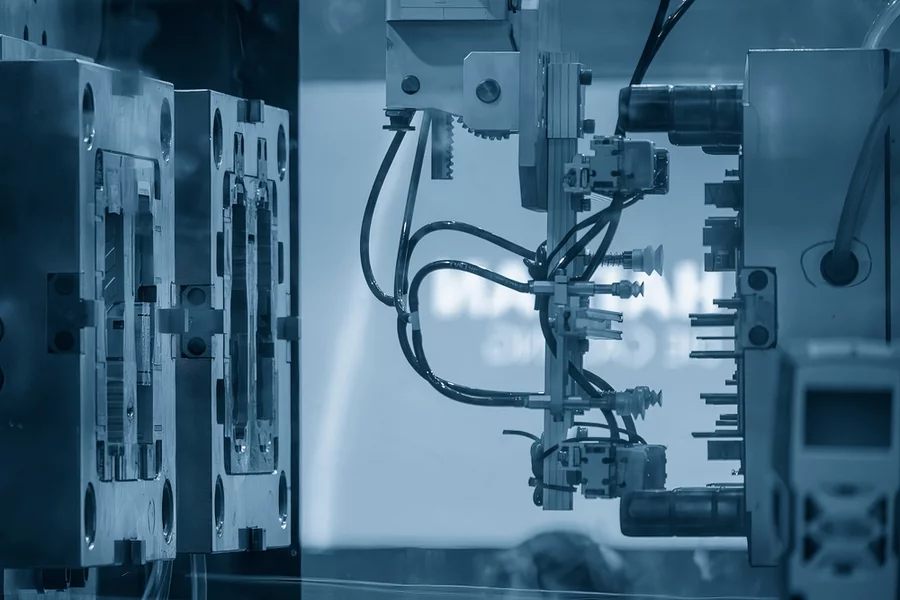
In hot runner injection molding, plastic remains molten as it flows through heated channels directly into the mold cavity. A typical hot runner system consists of manifolds, nozzle tips, heaters, temperature controllers and other critical hot runner components. These heated pathways allow molten plastic to flow efficiently into each mold cavity without creating runner waste.
By comparison, cold runner systems allow plastic to cool and solidify in the runner channels. By comparison, cold runner systems allow plastic in the runner channels to cool and solidify along with the molded parts. This creates additional material that may need to be separated and recycled or discarded, depending on the application. Although purging requirements vary by system design and processing conditions, hot runner systems can require additional care during purging to ensure that residual material is effectively removed from the manifold and nozzles.
Why Purging Hot Runners Is Different
Because plastic remains molten inside hot runner parts during normal operation, any residual resin or pigment can stay trapped in low-flow areas. During a color changeover, especially from dark to light colors, even tiny remnants can cause streaking, or contamination in the final molded part.
Properly learning how to purge hot runner systems ensures that old material is fully displaced before new production begins. This is critical when switching between different resins, additives and colors in plastic injection molds.
Best Practices to Purge Hot Runner Systems
To optimize color and material changes, follow these guidelines alongside the purge and equipment manufacturers’ instructions::
1. Stabilize processing conditions
Ensure temperatures, pressures, and screw speeds are stable before introducing purge material. Consistency helps the purge move evenly through all hot runner components.
2. Use a purge designed for hot runner technology
Not all purge materials are safe for hot runner systems. Choose a product that can safely pass through small gates without damaging tooling.
3. Maintain proper temperature
Where permitted by the purge, resin, and equipment manufacturers, raising temperatures slightly during the purging process can help improve flow and displacement. However, avoid excessive heat that could degrade the purge or resin.
4. Allow sufficient purge time
Purging hot runners can often take longer than cold runner systems because the material must travel through heated manifolds and nozzles before reaching the mold cavity.
5. Rinse thoroughly
After purging, introduce the new resin according to the recommended procedure and monitor the molded part closely until color and material consistency are achieved.
Hot Runners, Cold Runners, and Molded Part Quality
Whether you’re working with advanced hot runner technology or traditional cold runners, the goal is the same: clean transitions that protect part quality. A poorly purged hot runner can cause defects that repeat for hours, increasing scrap and downtime.
When done correctly, purging hot runner systems supports smoother changeovers, faster startups, and more consistent molded parts across production runs.
The Bottom Line
Hot runner systems offer tremendous efficiency benefits, but they demand a disciplined purging process during color and material changes. By understanding how hot runner systems work and applying proper purge techniques, processors can reduce contamination, protect tooling and keep production moving smoothly through repeated changeovers.